

How to Choose the Right Hot Melt Glue Nozzle for Your Production Line?
2026-09-16 10:46When a hot melt adhesive spraying system produces uneven glue patterns, excessive adhesive consumption, stringing, overspray, or frequent blockages, many manufacturers immediately suspect the hot melt glue machine.
But in a large number of production applications, the problem may start at a much smaller component:
the hot melt glue nozzle.
The nozzle determines how adhesive leaves the applicator and reaches the substrate. Its opening, spray pattern, flow capacity, operating temperature, installation position and compatibility with the adhesive can directly affect bonding quality and production stability.
For manufacturers using hot melt adhesive in mattress production, automotive interiors, packaging, leather goods, footwear, composite lamination, edge banding, profile wrapping, courier bags, handle bags, bookbinding and air filter manufacturing, choosing the right nozzle is therefore not simply a spare-parts decision.
It is a process engineering and procurement decision.
So, how should a factory choose the right hot melt glue nozzle?
The practical answer is:
Select the nozzle according to the adhesive, application pattern, required glue output, substrate, production speed and hot melt equipment—not according to nozzle price alone.
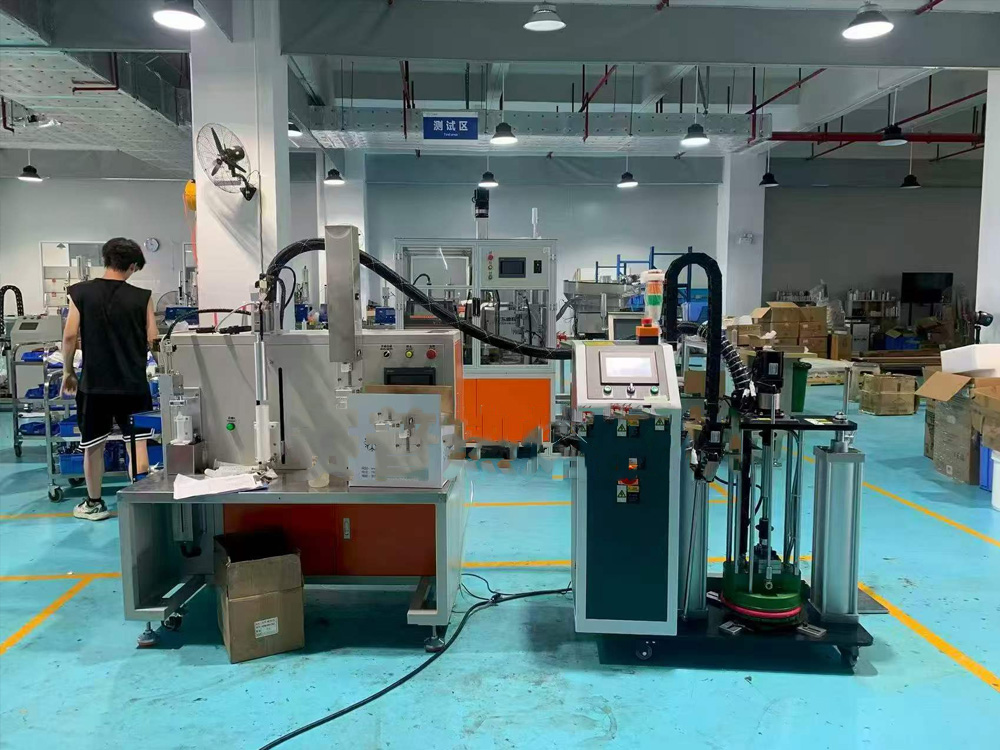
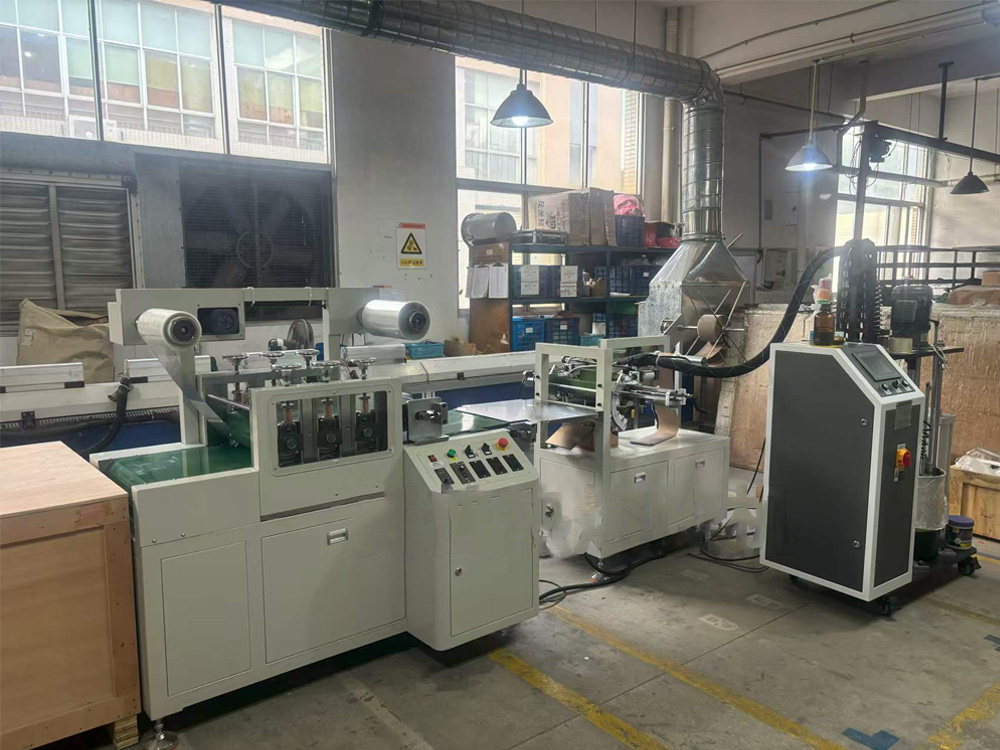
Saipu Electromechanical Device Co., Ltd. provides hot melt adhesive spraying equipment and application-oriented bonding solutions for manufacturers across multiple industries. Its equipment configurations can be matched with different adhesive application requirements, including spray, bead, line and other hot melt dispensing processes.
1. The First Question: What Adhesive Application Pattern Do You Need?
Before selecting a nozzle, determine what the adhesive needs to look like on the substrate.
Different production processes may require completely different application patterns.
Common hot melt adhesive application patterns
| Application pattern | Typical requirement | Suitable applications |
|---|---|---|
| Spiral spray | Wide, flexible adhesive distribution | Mattress, textile, upholstery |
| Random spray | Irregular but controlled coverage | Automotive interiors, furniture |
| Flat spray | Wider and relatively uniform coverage | Lamination, composite materials |
| Bead | Concentrated adhesive line | Packaging, assembly |
| Multi-line | Several parallel adhesive lines | Lamination, filter manufacturing |
| Dot application | Controlled adhesive points | Small components, assembly |
| Intermittent spray | Adhesive applied according to product position | Packaging, automated assembly |
| Wide coating | Large-area adhesive coverage | Film, textile and composite lamination |
The first mistake many buyers make is purchasing a nozzle based only on its physical dimensions.
The better approach is to define the required adhesive pattern first.
For example, a mattress factory may need a broad spiral spray pattern, while a packaging line may require a precise bead.
Using the same nozzle configuration for both applications can result in unnecessary adhesive consumption or insufficient bonding.
2. Match the Nozzle to the Hot Melt Adhesive
The nozzle is in direct contact with the adhesive, so adhesive characteristics must be considered before selecting the nozzle.
Important parameters include:
Adhesive type
Viscosity
Processing temperature
Melting characteristics
Adhesive flow rate
Pressure requirement
Reactive or non-reactive chemistry
Presence of fillers or additives
Common industrial hot melt adhesive categories include:
EVA hot melt adhesive
PSA hot melt adhesive
PUR hot melt adhesive
PO hot melt adhesive
Other specialty hot melt formulations
These materials do not necessarily behave the same way during dispensing.
Why viscosity matters
A high-viscosity adhesive requires a different flow condition from a relatively low-viscosity adhesive.
If the nozzle orifice is too small for the adhesive and required output, the system may experience:
High flow resistance → increased pressure → unstable output → poor spray pattern → nozzle blockage
If the nozzle opening is excessively large, the opposite problem can occur:
Excessive glue output → higher adhesive consumption → overspray → increased production cost
Therefore, nozzle selection should be based on the relationship between:
Viscosity + Temperature + Pressure + Nozzle Opening + Required Flow Rate
3. How Does Nozzle Opening Size Affect Glue Output?
Nozzle orifice size is one of the most important selection parameters.
A smaller opening generally provides more concentrated adhesive delivery, while a larger opening can accommodate higher flow requirements.
However, the relationship is not simply:
Bigger nozzle = better performance.
Actual adhesive output also depends on:
Adhesive viscosity
Pump performance
System pressure
Adhesive temperature
Nozzle geometry
Spray air, where applicable
Application distance
Adhesive formulation
For this reason, a factory should not select a nozzle solely according to its diameter.
Instead, provide the equipment supplier with the required glue consumption and production speed.
For example:
Required adhesive output = adhesive consumption per product × production quantity per hour
This provides a much better basis for nozzle selection.
4. Spray Width Is Just as Important as Glue Output
A nozzle can deliver the correct amount of adhesive and still produce a poor bonding result if the spray width is wrong.
Consider a mattress production line.
If the required adhesive coverage is wide but the spray pattern is too narrow, the operator may compensate by:
Increasing adhesive output
Slowing down the conveyor
Adding additional spray passes
All three can increase production cost.
The same problem can occur in automotive interior lamination.
When selecting a spray nozzle, define:
Required spray width
Distance between nozzle and substrate
Production line speed
Number of nozzles
Overlap between spray patterns
Adhesive application weight
Substrate width
A well-designed spray system should match the nozzle configuration with the actual production width.
5. Consider Production Speed Before Selecting the Nozzle
A nozzle that performs well during a laboratory test may not perform the same way on a high-speed production line.
Production speed changes the amount and distribution of adhesive applied to the substrate.
For example:
Low-speed production
The nozzle has more time to deposit adhesive on a specific area.
High-speed production
The system needs sufficient adhesive output and an appropriate spray width to maintain the required application weight.
Therefore:
Nozzle selection = Nozzle capacity + Production speed + Spray width + Required adhesive weight
For automated production, buyers should provide the supplier with actual line-speed information rather than simply saying “high-speed production.”
6. Choose the Nozzle According to the Substrate
The same adhesive pattern may not be suitable for every material.
Different substrates have different surface characteristics and bonding requirements.
Typical industrial substrates include:
Foam
Fabric
Nonwoven
Leather
Synthetic leather
Plastic
Metal
Wood
Paper
Film
Composite materials
A porous substrate may require a different adhesive distribution from a smooth plastic film.
For example, in mattress manufacturing, the adhesive may need to cover a relatively large area while maintaining flexibility.
In automotive interiors, the adhesive pattern may need to provide sufficient bonding without visible adhesive breakthrough.
In packaging, the priority may be rapid, controlled bonding with minimal excess glue.
This is why nozzle selection should always consider the substrate + adhesive + application method as one system.
7. How to Choose Between Spray, Bead and Other Nozzle Types?
7.1 Spray Nozzle
Spray nozzles are suitable when adhesive needs to be distributed over a wider area.
Typical applications include:
Mattresses
Automotive interiors
Furniture
Upholstery
Textile lamination
Composite bonding
The objective is usually not to produce the largest possible glue output.
It is to achieve the required coverage with controlled adhesive consumption.
7.2 Bead Nozzle
A bead nozzle delivers adhesive in a relatively concentrated line.
It can be suitable for:
Packaging
Assembly
Bookbinding
Edge bonding
Component bonding
Certain filter applications
The key parameters are:
Bead width
Bead continuity
Glue output
Line speed
Start/stop response
For automated lines, clean adhesive shutoff can also be important because excessive residual adhesive can create stringing and contamination.
7.3 Multi-Nozzle Configuration
For wide products or multiple adhesive lines, several nozzles may be installed on one applicator system.
This can provide:
Wider application coverage
Multiple adhesive lines
Flexible process configuration
Higher production capacity
However, the nozzles should be balanced so that each outlet delivers the required adhesive quantity.
Otherwise, the production line may experience:
Uneven output between nozzles → inconsistent bonding → product defects
8. Temperature Compatibility Is Critical
Hot melt adhesive must remain within its appropriate processing temperature range while traveling through the system.
The nozzle is the final point in the heated adhesive path.
If the adhesive temperature at the nozzle is too low, viscosity may increase.
This can lead to:
Poor flow
Incomplete spraying
Narrow spray pattern
Increased pressure
Nozzle blockage
If the temperature is unnecessarily high, some adhesives may experience degradation or excessive thermal exposure.
Therefore, the correct question is not:
“What is the highest temperature the nozzle can withstand?”
The better question is:
“Can the nozzle and applicator maintain the adhesive manufacturer's recommended processing condition during actual production?”
The nozzle, heated hose, applicator and melter should therefore be treated as a complete thermal system.
9. PUR Hot Melt Adhesive Requires Additional Attention
PUR hot melt adhesive is widely used where manufacturers require strong and durable bonding.
However, reactive PUR is different from conventional thermoplastic hot melt adhesive because it reacts with moisture during curing.
This means the equipment and operating procedure should consider:
Adhesive exposure to ambient moisture
Sealing of the adhesive supply
Heated hose condition
Nozzle cleanliness
Shutdown procedure
Adhesive residence time
Cured adhesive residue
If cured material reaches a small nozzle opening, blockage can occur quickly.
Therefore, when purchasing a PUR hot melt glue machine, the nozzle should not be considered independently.
The complete system should be evaluated:
PUR adhesive container → Melting system → Pump → Filter → Heated hose → Applicator → Nozzle
This is particularly important for factories operating PUR equipment for long periods or under frequent production interruptions.
10. How Can the Wrong Nozzle Increase Adhesive Consumption?
Nozzle selection directly influences how efficiently adhesive is distributed.
Suppose a production line requires a defined adhesive application weight.
If the nozzle produces excessive output, the operator may compensate by:
Reducing pressure
Increasing line speed
Reducing temperature
Increasing spray distance
These adjustments may change the application pattern rather than solving the fundamental problem.
Excess adhesive can create:
Higher material cost + longer curing time + contamination + overspray + additional cleaning
The correct nozzle should therefore deliver enough adhesive to achieve the required bond without creating unnecessary excess.
For procurement teams, a useful KPI is:
Adhesive consumption per product
For example:
kg of adhesive / 1,000 products
This is often more meaningful than simply comparing the nominal maximum output of two machines.
11. What Causes Stringing and Overspray?
Stringing and overspray are common concerns in hot melt adhesive dispensing.
However, they are not necessarily caused by the nozzle alone.
Possible factors include:
Incorrect adhesive temperature
Excessive pressure
Incorrect nozzle geometry
Poor nozzle shutoff
Excessive application distance
Incorrect adhesive viscosity
Adhesive formulation
Production speed
Inappropriate spray-air settings, where applicable
This is why changing the nozzle without checking the rest of the process may not solve the problem.
A proper technical evaluation should examine:
Adhesive + Temperature + Pressure + Nozzle + Distance + Speed + Substrate
12. Procurement Checklist: 10 Questions to Ask Your Hot Melt Nozzle Supplier
Before ordering hot melt nozzles, procurement managers should provide the supplier with specific production information.
1. What adhesive are you using?
Specify EVA, PUR, PSA, PO or another formulation.
2. What is the adhesive viscosity?
Provide the manufacturer's technical data where available.
3. What is the recommended processing temperature?
Do not select the nozzle based on temperature alone.
4. What adhesive output is required?
Provide kg/h, g/product or another measurable value.
5. What spray or bead width is required?
The supplier needs actual application dimensions.
6. What is the production line speed?
Specify m/min, products/min or another measurable parameter.
7. What substrate are you bonding?
For example:
Foam + fabric is different from plastic + metal.
8. Is the application continuous or intermittent?
Frequent start/stop operation requires suitable adhesive shutoff performance.
9. How many adhesive lines are required?
This determines whether a single, dual or multi-outlet configuration is appropriate.
10. Can the nozzle be tested with your actual adhesive?
This is one of the most valuable questions.
A nozzle that looks suitable on paper may perform differently with the customer's actual adhesive, substrate and production speed.
13. A Practical Nozzle Selection Process
For factories that are unsure which hot melt nozzle to purchase, the following process is more reliable than selecting by price.
Step 1: Identify the adhesive
EVA / PUR / PSA / PO / Other
↓
Step 2: Identify the application
Spray / Spiral / Bead / Line / Dot / Coating
↓
Step 3: Define the production speed
m/min or products/hour
↓
Step 4: Define adhesive consumption
g/product or kg/h
↓
Step 5: Define application width
mm or product width
↓
Step 6: Confirm temperature and pressure conditions
Ensure compatibility with the adhesive and hot melt equipment.
↓
Step 7: Select nozzle configuration
Choose the appropriate nozzle geometry, opening, number of outlets and installation configuration.
↓
Step 8: Conduct an actual adhesive trial
Evaluate:
Spray pattern
Adhesive consumption
Bonding quality
Stringing
Overspray
Start/stop performance
Continuous production stability
This final step is critical.
The best nozzle is not necessarily the nozzle with the largest output or lowest purchase price. It is the nozzle that delivers the required adhesive pattern consistently at the lowest practical process cost.
14. How Saipu Helps Manufacturers Match Nozzles With Hot Melt Equipment
Saipu Electromechanical Device Co., Ltd. does not treat the nozzle as an isolated spare component.
For industrial hot melt adhesive applications, the nozzle needs to work together with the entire adhesive delivery system.
Saipu's technical approach considers:
Adhesive
What adhesive is being processed and what are its recommended operating conditions?
Production
How fast does the production line run?
Application
Does the customer require spray, spiral spray, bead, line or another application pattern?
Substrate
What materials need to be bonded?
Adhesive quantity
How much adhesive is required per product or per hour?
Equipment
What melting, pumping, heating, filtration and control configuration is required?
Automation
Does the applicator need to communicate with a conveyor, robot, PLC or other production equipment?
This approach helps avoid a common purchasing mistake:
Buying a nozzle first and trying to make the production process fit it afterward.
Instead, the equipment should be configured around the actual bonding process.
15. Where Can the Right Hot Melt Nozzle Make the Biggest Difference?
Mattress Manufacturing
A suitable spray configuration can help distribute adhesive over foam and fabric surfaces while controlling adhesive consumption.
Automotive Interior
Controlled adhesive distribution is important for bonding fabrics, acoustic materials, trim components and other interior materials.
Packaging
Bead or controlled spray application can support high-speed bonding while reducing unnecessary adhesive deposition.
Leather and Footwear
The nozzle should match the required coverage and substrate geometry to avoid excessive adhesive application.
Composite Lamination
Uniform adhesive distribution is important for bonding films, fabrics, nonwovens and other layered materials.
Edge Banding and Profile Wrapping
Stable adhesive delivery helps maintain consistent bonding along continuous profiles and furniture components.
Courier Bags and Handle Bags
The application system needs to respond to high-speed production and intermittent bonding positions.
Bookbinding
Controlled adhesive lines and reliable start/stop performance can be important for automated book production.
Air Filters
The nozzle configuration should match the required adhesive line, bead or spray pattern and production speed.
16. FAQ: Choosing a Hot Melt Glue Nozzle
What is the most important factor when choosing a hot melt glue nozzle?
There is no single parameter. The nozzle should be selected according to adhesive type, viscosity, required flow rate, application pattern, spray width, production speed and substrate.
Can one hot melt nozzle be used for different adhesives?
Sometimes, but compatibility must be confirmed. Different adhesives can have different viscosity, temperature and flow characteristics. A nozzle that works well with one formulation may not provide the same result with another.
Does a larger nozzle always provide more glue?
A larger opening can support greater flow, but actual adhesive output also depends on pressure, viscosity, temperature, pump capacity and nozzle geometry.
Why is my hot melt spray pattern uneven?
Possible causes include partial nozzle blockage, unstable temperature, pressure fluctuation, unsuitable viscosity, incorrect spray distance, worn components or an inappropriate nozzle configuration.
How often should a hot melt nozzle be replaced?
There is no universal replacement interval. It depends on adhesive type, operating temperature, production hours, contamination, maintenance and nozzle wear. Monitor spray quality and output rather than replacing components only according to calendar time.
Can the wrong nozzle cause adhesive waste?
Yes. An unsuitable nozzle can produce excessive output, poor coverage or overspray, all of which may increase adhesive consumption.
Is a special nozzle required for PUR hot melt adhesive?
PUR applications require equipment and components compatible with the adhesive's processing conditions and moisture-reactive characteristics. The complete adhesive delivery system should be evaluated rather than selecting the nozzle independently.
Should I test a nozzle before purchasing?
Yes. Whenever possible, test the nozzle with the actual adhesive, substrate, application pattern and production speed. This provides much more useful information than comparing nozzle specifications alone.
17. Final Procurement Advice
Choosing a hot melt glue nozzle should not begin with:
“How much does this nozzle cost?”
It should begin with:
“What adhesive pattern does my production process actually require?”
Then work backward from the production requirements:
Application pattern → Adhesive → Viscosity → Flow rate → Spray width → Production speed → Temperature → Pressure → Nozzle configuration
This process helps manufacturers avoid common problems such as:
Uneven spraying
Excessive adhesive consumption
Overspray
Stringing
Incomplete bonding
Frequent nozzle blockage
Unstable glue output
Unplanned production downtime
For factories working with mattresses, automotive interiors, packaging, leather goods, footwear, composite materials, edge banding, profile wrapping, courier bags, handle bags, bookbinding or air filters, nozzle selection should be integrated into the complete hot melt adhesive equipment design.
Saipu Electromechanical Device Co., Ltd. provides hot melt adhesive spraying machinery and one-stop bonding solutions designed around different industrial production requirements.
If your factory is experiencing uneven spray patterns, nozzle clogging, excessive glue consumption, unstable adhesive output or frequent production stops, provide your adhesive type, viscosity, required glue consumption, application width, production speed and substrate information. Saipu can then evaluate the hot melt adhesive delivery and nozzle configuration according to your actual process.